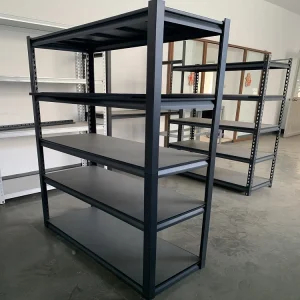
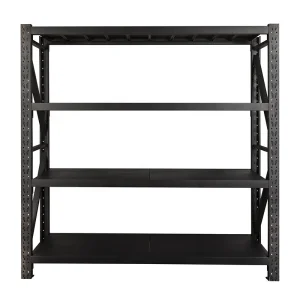
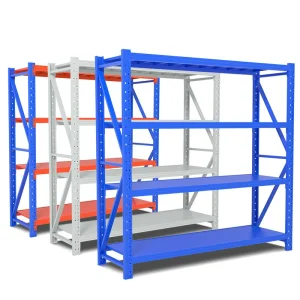
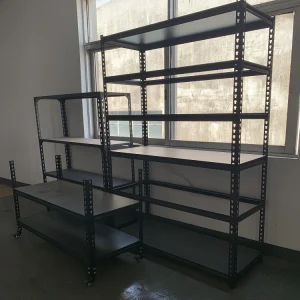
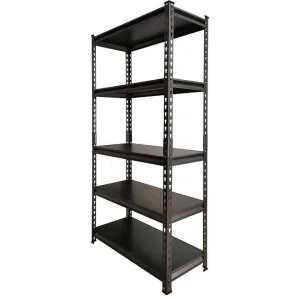
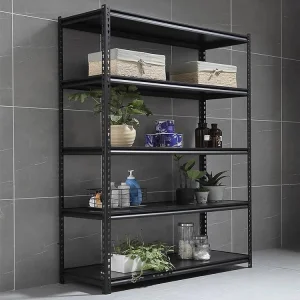
Explore our comprehensive range of high-performance, corrosion-resistant, and precision-engineered metal storage solutions designed for global warehouses, distribution networks, and modern fulfillment hubs.
In the current landscape of global commerce, supply chain resilience depends on high-performance warehouse management infrastructure. Enterprises worldwide face escalating pressures to maximize cubic storage capacity, accelerate inventory throughput, and minimize operational expenditure.
Third-party logistics providers require modular, highly adaptable racking systems that can be swiftly reconfigured to accommodate fluctuating client inventory profiles, seasonal surges, and high-density SKU management.
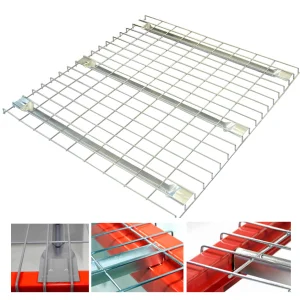
With rapid order-to-delivery cycles, e-commerce giants demand multi-tier shelving, boltless rivet racks, and wire mesh decking designed for lightning-fast pick-and-pack operations and automated guided vehicle (AGV) integration.
Heavy-duty industrial storage racks and reinforced structural steel framing ensure safe, organized containment of raw materials, heavy components, and finished goods under rigorous shop-floor conditions.
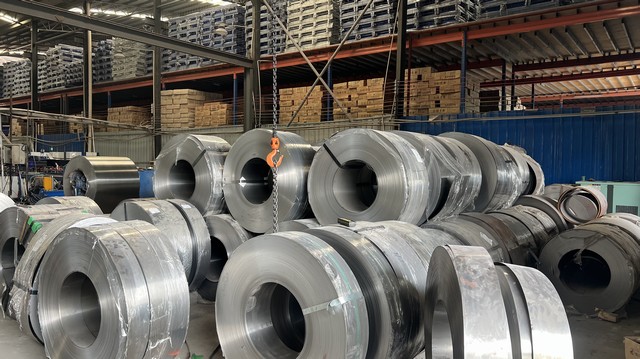
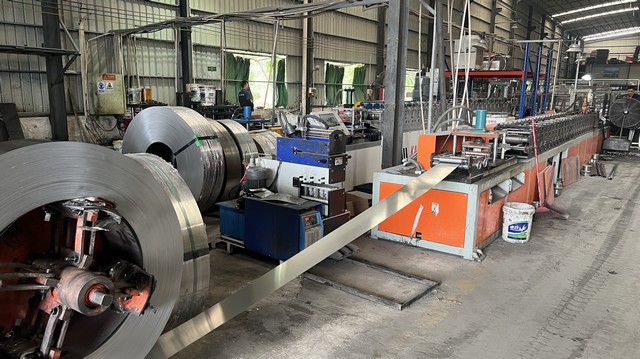
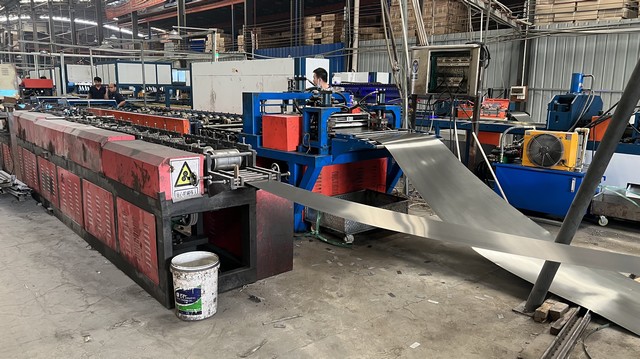
Our manufacturing ecosystem integrates advanced metallurgy, automated cold-rolling technology, and rigorous anti-corrosion treatments to deliver industry-leading structural performance.
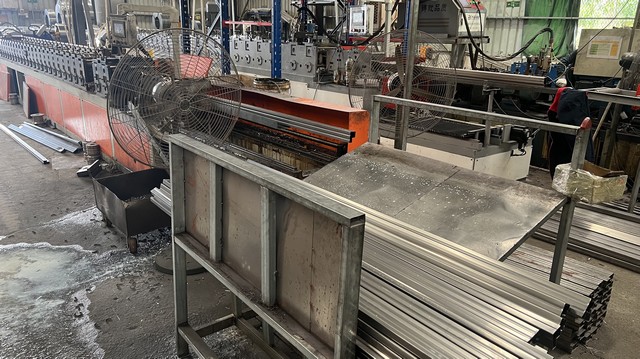
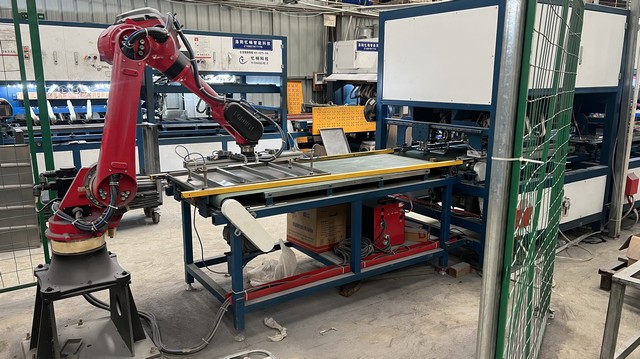
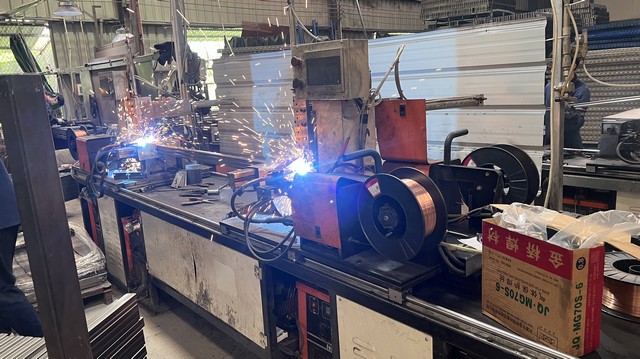
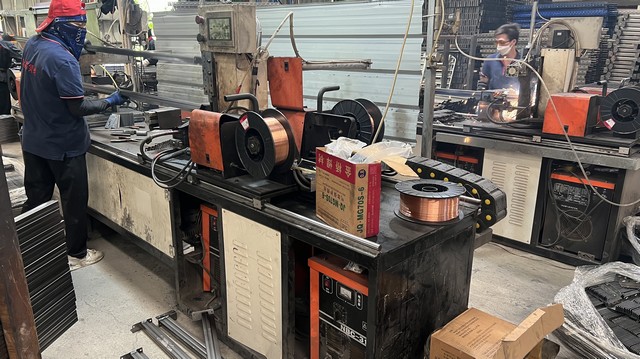
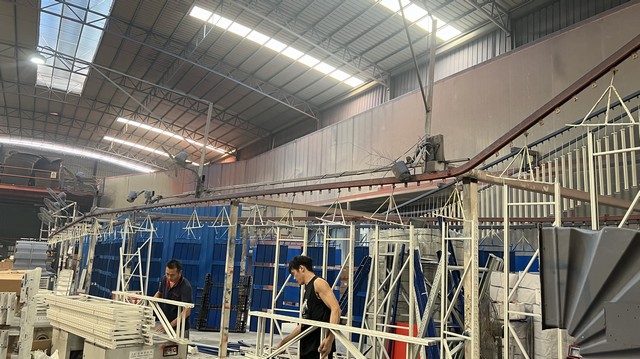
Shenzhen Aliracking Industry Co., Ltd. was established in 2015 with a clear vision: to revolutionize warehouse management hardware through precision engineering. Operating from our expansive 35,000 m² manufacturing plant equipped with square tube rolling lines, fully automatic rolling production lines, dedicated welding systems, and electrostatic powder coating lines, we maintain complete vertical integration.
Quality and structural integrity remain non-negotiable pillars of our operations. We implement stringent ISO 9001 certified Quality Assurance (QA) protocols, complemented by comprehensive Third-Party On-Site Inspections and Non-Destructive Testing (NDT) for all load-bearing components. Guided by our team of 28 QA/QC specialists and 15 dedicated R&D engineers—who successfully engineered 45 new product designs last year—we deliver custom dimensions, tailored load ratings, and specialized powder-coated finishes that satisfy the most demanding global specifications.
Continuing our extensive catalog offerings for enterprise-grade warehouse organization, heavy-duty storage, and commercial retail applications.
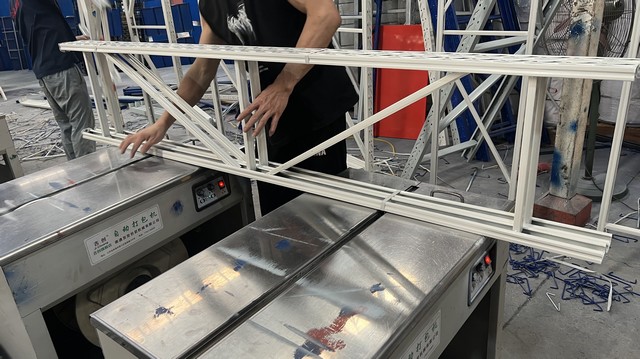
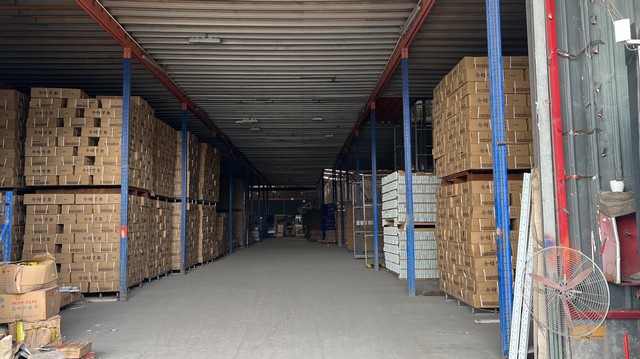
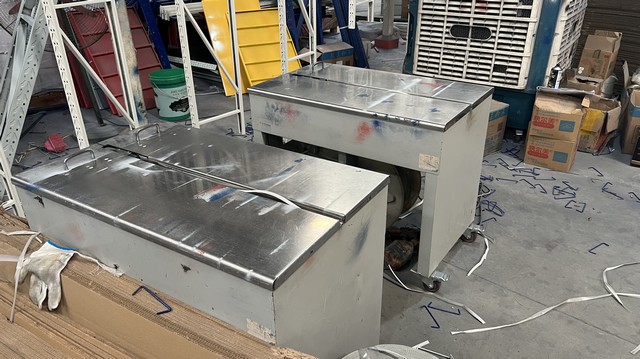
Transparency in production excellence. Witness our precision fabrication processes from raw material preparation to final warehouse dispatch.
Expert answers regarding our warehouse management hardware, manufacturing capabilities, and global procurement procedures.
With over 12 years of industry experience and 8 years of direct export expertise, we operate a 35,000 m² factory backed by 850+ supply chain partners. Our rigorous ISO 9001 quality standards, dedicated R&D engineering team, and robust annual export revenue of $18 million prove our capability to handle large-scale international enterprise orders seamlessly.
Yes. Our 15 in-house R&D engineers specialize in OEM and ODM services. We can tailor structural dimensions, upright gauges, beam lengths, tier counts, and electrostatic powder coating colors to match your precise facility requirements and load-bearing specifications.
All our steel products undergo thorough surface preparation followed by advanced electrostatic powder coating or hot-dip galvanization (such as for wire mesh decking). This ensures superior resistance against rust, abrasion, and harsh environmental conditions in industrial warehouses and distribution hubs.
We maintain a robust global footprint, regularly exporting to major logistics hubs and industrial enterprises across North America, Europe, Southeast Asia, and the Middle East, serving top-tier 3PL providers, e-commerce fulfillment centers, and large distributors.
 Aliracking