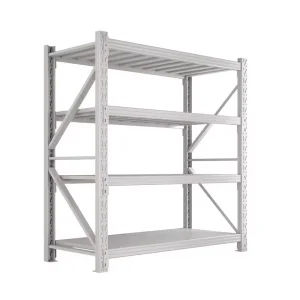
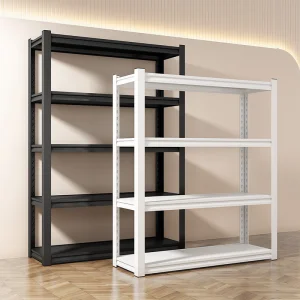
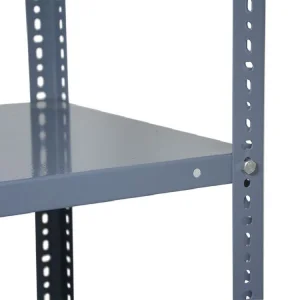
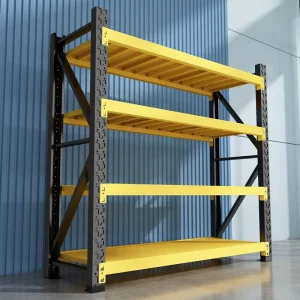
Explore our flagship high-load capacity storage units, engineered with advanced anti-corrosion electrostatic powder coating for ultimate commercial and warehouse durability.
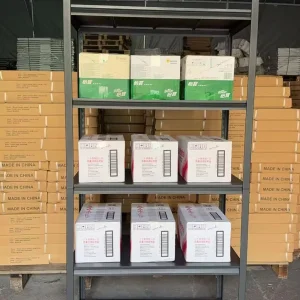
A comprehensive analytical overview of macro-level industrial storage developments, global procurement patterns, and technological milestones shaping modern supply chains.
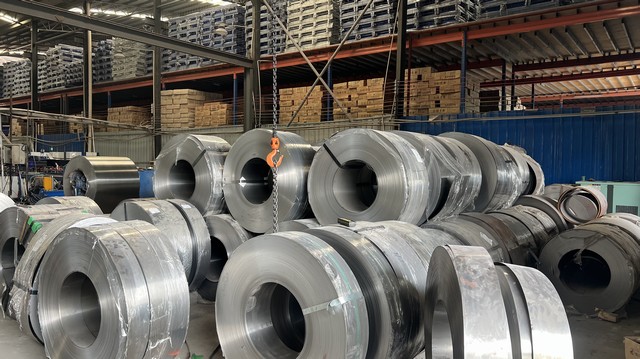
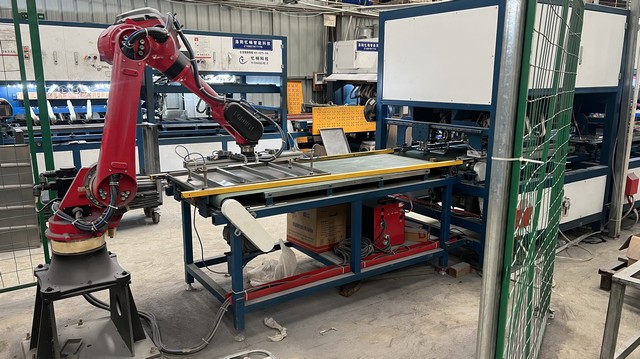
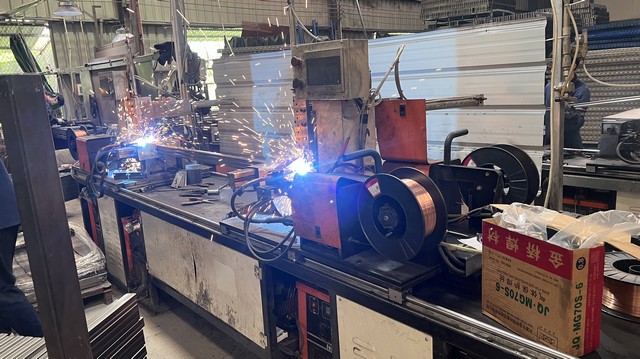
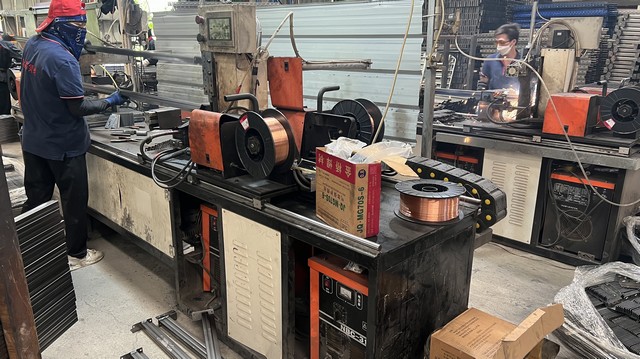
The global warehousing and drum containment sectors are experiencing a seismic shift toward modularity, heavy-duty load optimization, and automated compatibility. As chemical processing, oil & gas, and manufacturing sectors scale operations, traditional static shelving is being phased out in favor of engineered custom OEM drum racks. Modern facilities demand smart storage architecture featuring high-grade cold-rolled steel, automated robotic welding joints, and specialized anti-corrosion electrostatic coatings capable of withstanding aggressive industrial environments.
International buyers—ranging from Fortune 500 3PL providers to massive e-commerce fulfillment hubs—increasingly prioritize direct factory partnerships over traditional tier-1 distributors. Key purchasing criteria center on stringent quality assurance (ISO 9001, CE certifications), third-party on-site structural inspections, NDT (Non-Destructive Testing) verification for load-bearing components, and robust supply chain resilience capable of sustaining multi-million dollar annual order volumes without delivery friction.
Compliance with regional safety regulations (such as OSHA guidelines in North America and EN standards in Europe) is non-negotiable. Leading Chinese manufacturers bridge regulatory divides by offering full-scale compliance documentation, localized engineering consultation, seismic load simulations, and custom dimensional configurations tailored to specific regional warehouse footprints and hazardous material containment mandates.
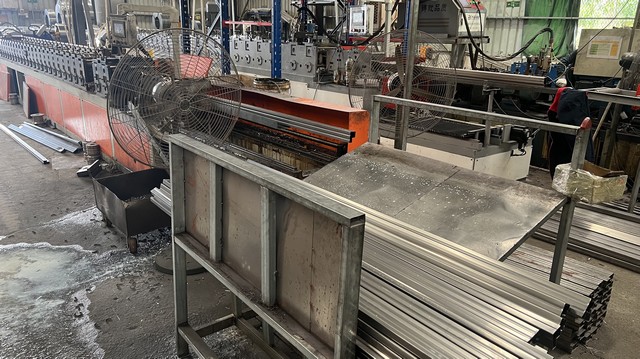
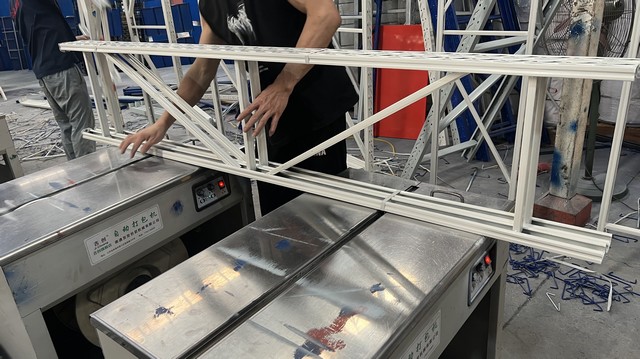
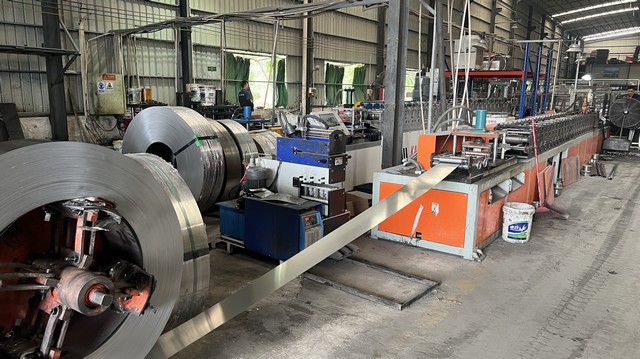
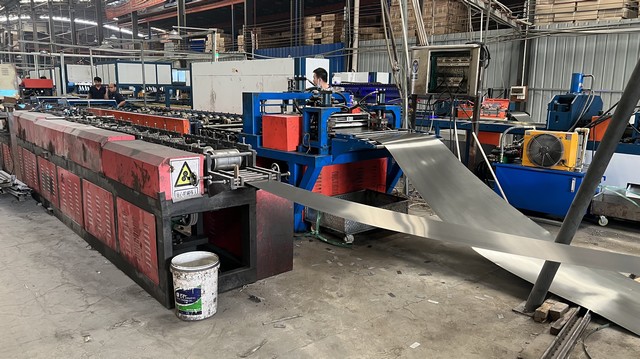
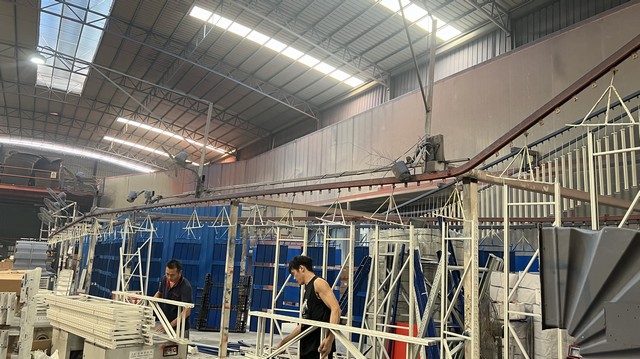
Looking toward the horizon, the integration of IoT-enabled weight sensors, automated storage and retrieval systems (AS/RS) compatibility, and sustainable green manufacturing processes represent the vanguard of drum rack engineering. Automated fully rolling production lines and precision powder-coating chambers ensure zero-defect output, reducing carbon footprints while maximizing structural longevity under extreme cyclic loads.
Shenzhen Aliracking Industry Co., Ltd. represents the absolute pinnacle of structural steel fabrication and warehouse optimization engineering.
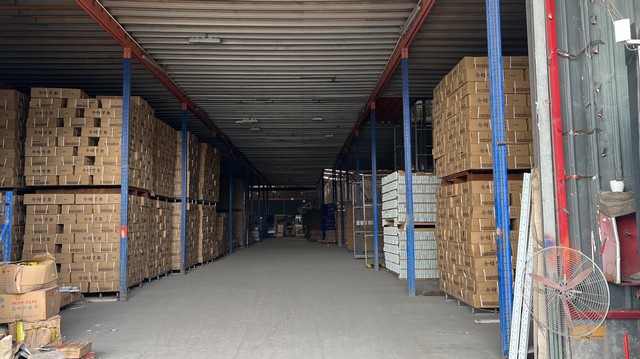
Shenzhen Aliracking Industry Co., Ltd. is a leading manufacturer specializing in high-performance warehouse racking and industrial storage solutions. Established in 2015, the company operates a state-of-the-art production facility covering an expansive area of 35,000 m². With over 12 years of industry experience and 8 years of direct export expertise, we deliver robust, high-density storage systems to businesses worldwide, generating an annual export revenue of $18 million.
Quality and safety are at the core of our manufacturing philosophy. We implement rigorous ISO 9001 certified Quality Assurance (QA) protocols alongside comprehensive Third-Party On-Site Inspections and Non-Destructive Testing (NDT) for load-bearing components. Supported by a dedicated team of 28 QA/QC specialists and 15 R&D engineers, we released 45 new product designs last year alone. Our strong engineering capability allows us to offer extensive customization options, including tailored structural dimensions, customized load capacities, specialized powder coatings, and OEM/ODM services to meet complex logistics demands.
Backed by a solid Foreign Trade Corporation background and a strong network of over 850 supply chain partners, Shenzhen Aliracking serves a global customer base across North America, Europe, Southeast Asia, and the Middle East. Our primary clients include 3PL Logistics Providers, E-commerce Fulfillment Centers, Large Distribution Warehouses, and Industrial Manufacturers. We remain committed to optimizing space utilization and improving operational efficiency for warehousing enterprises across the globe.
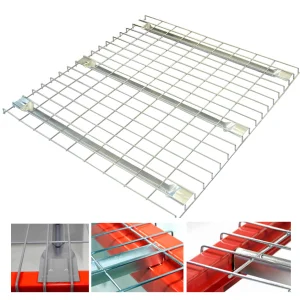
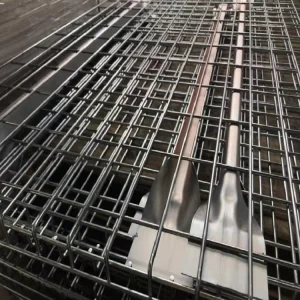
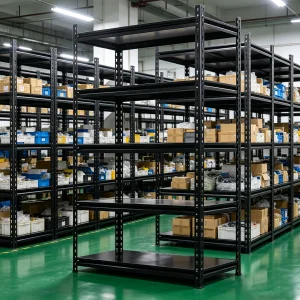
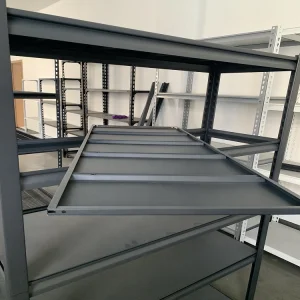
Discover our extended inventory of anti-rust adjustable racks, high-strength wire mesh decking, and super heavy-duty commercial storage configurations.
Expert answers regarding custom manufacturing, load capacities, international shipping, and quality compliance for industrial storage systems.
 Aliracking