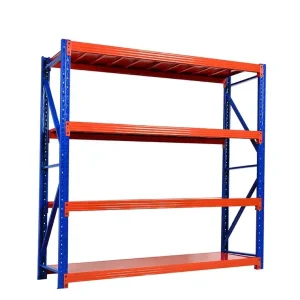
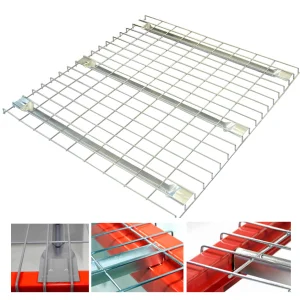
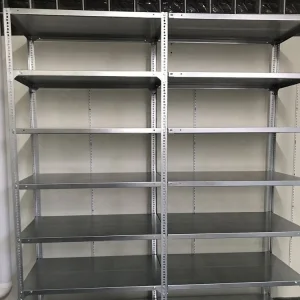
Explore our flagship heavy-duty racks, medium-duty shelving, and corrosion-protected logistics equipment engineered for demanding industrial environments.
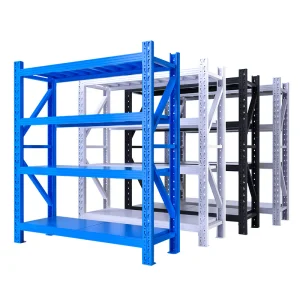
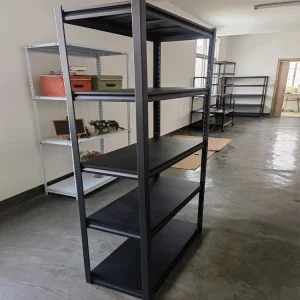
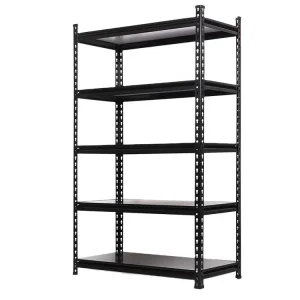
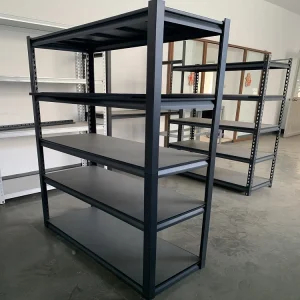
Deep dive into Shenzhen Aliracking Industry Co., Ltd. — Setting global benchmarks in logistics equipment manufacturing with uncompromising quality standards.
Shenzhen Aliracking Industry Co., Ltd. is a leading manufacturer specializing in high-performance warehouse racking and industrial storage solutions. Established in 2015, the company operates a state-of-the-art production facility covering an expansive area of 35,000 m². With over 12 years of industry experience and 8 years of direct export expertise, we deliver robust, high-density storage systems to businesses worldwide, generating an annual export revenue of $18 million.
Quality and safety are at the core of our manufacturing philosophy. We implement rigorous ISO 9001 certified Quality Assurance (QA) protocols alongside comprehensive Third-Party On-Site Inspections and Non-Destructive Testing (NDT) for load-bearing components. Supported by a dedicated team of 28 QA/QC specialists and 15 R&D engineers, we released 45 new product designs last year alone. Our strong engineering capability allows us to offer extensive customization options, including tailored structural dimensions, customized load capacities, specialized powder coatings, and OEM/ODM services to meet complex logistics demands.
Backed by a solid Foreign Trade Corporation background and a strong network of over 850 supply chain partners, Shenzhen Aliracking serves a global customer base across North America, Europe, Southeast Asia, and the Middle East. Our primary clients include 3PL Logistics Providers, E-commerce Fulfillment Centers, Large Distribution Warehouses, and Industrial Manufacturers. We remain committed to optimizing space utilization and improving operational efficiency for warehousing enterprises across the globe.
Discover our comprehensive boltless rivet shelving, multi-level structural steel racks, and heavy-duty carbon steel warehousing systems.
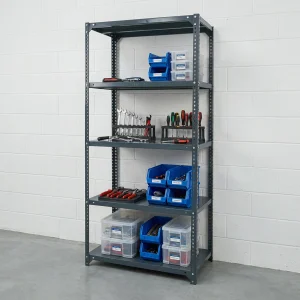
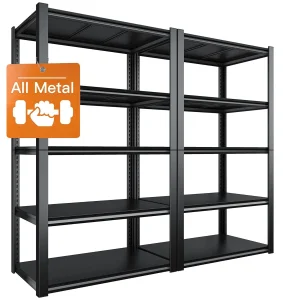
Navigating the digital transformation of modern warehousing through smart automation, IoT-enabled racking, and green manufacturing.
As global supply chains transition toward Industry 4.0, logistics equipment manufacturers must evolve beyond static structural steel. At Aliracking, our R&D roadmap incorporates smart sensors embedded within upright columns and cross-beams, enabling real-time structural health monitoring and load-capacity tracking.
By integrating RFID and IoT telemetry into our multi-level rack systems, warehouse managers can instantly track inventory turnover velocities and prevent structural overloading before safety thresholds are breached.
Sustainability is no longer optional in global procurement. Our electrostatic powder coating lines utilize zero-VOC, environmentally friendly finishes that extend corrosion resistance by up to 200%. Furthermore, our cold-rolled steel fabrication processes minimize scrap metal generation, achieving a closed-loop recycling rate exceeding 95% across our 35,000 m² facility.
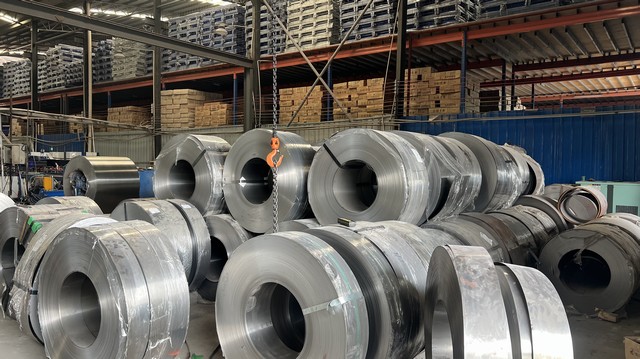
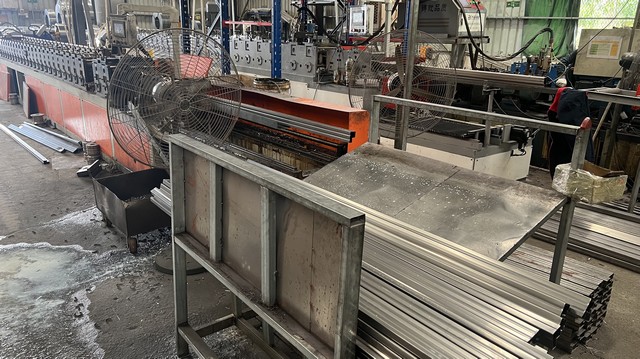
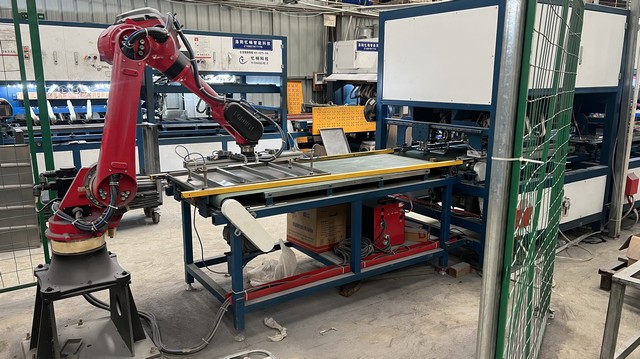
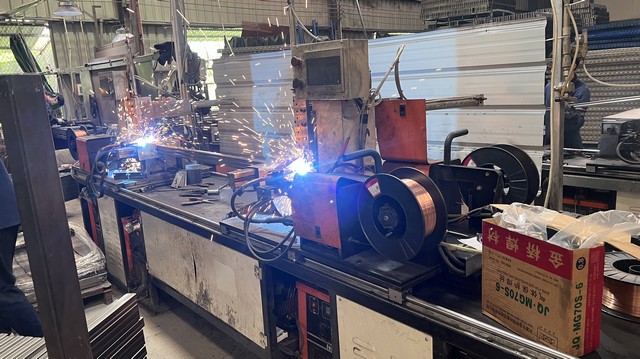
A transparent look into our state-of-the-art machinery, automated rolling lines, and precision welding workshops.
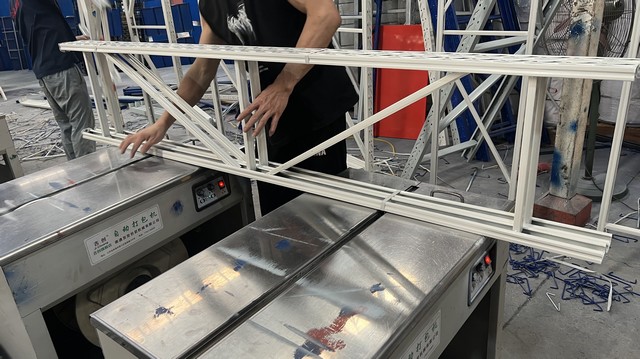
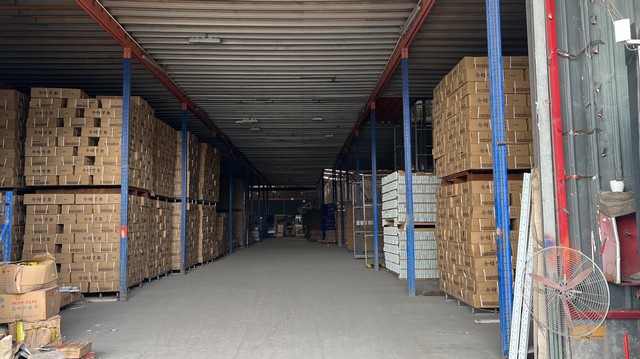
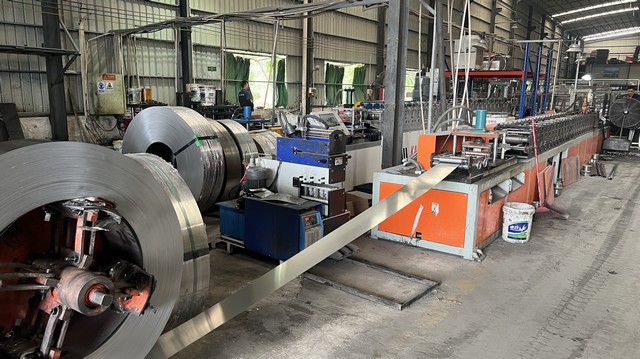
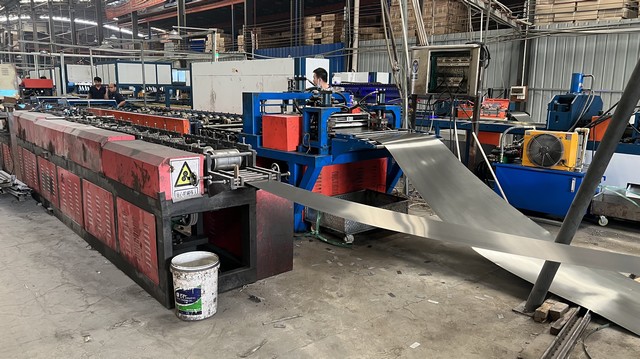
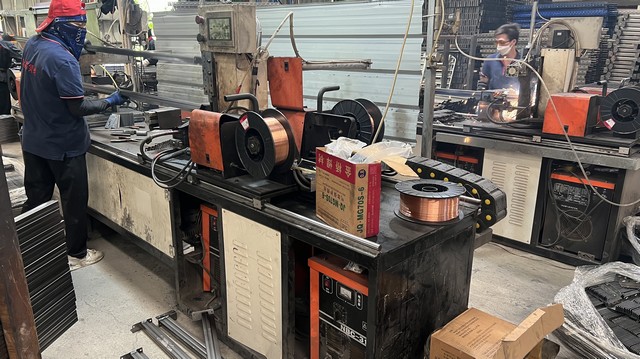
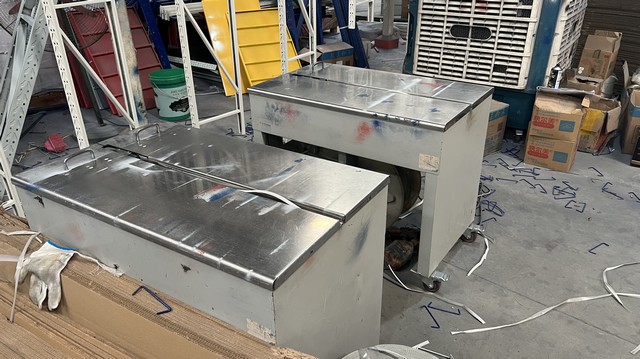
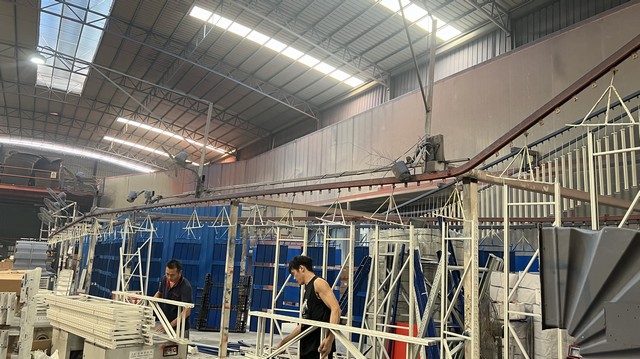
Understanding why global enterprises rely on Chinese manufacturing hubs for robust, cost-effective, and scalable logistics infrastructure.
The global industrial landscape demands rapid deployment times and cost predictability. China's manufacturing ecosystem—particularly in industrial hubs like Shenzhen—provides an unrivaled network of raw material suppliers, automated component fabricators, and specialized logistics corridors.
At Aliracking, our integration with over 850 vetted supply chain partners enables us to absorb market volatility, secure premium-grade cold-rolled steel at competitive costs, and maintain strict adherence to international delivery timelines without compromising structural integrity.
Expert answers regarding our manufacturing capabilities, compliance certifications, and global shipping policies.
Our product range accommodates diverse operational needs, from light-duty 100kg boltless rivet shelves to heavy-duty carbon steel warehouse systems supporting up to 1000kg per tier.
Yes. With 15 specialized R&D engineers, we provide fully tailored structural dimensions, customized load configurations, specialized electrostatic powder coatings, and private-label packaging.
All manufacturing processes strictly follow ISO 9001 Quality Assurance protocols, supplemented by rigorous third-party on-site inspections and non-destructive testing (NDT).
We serve a worldwide client base across North America, Europe, Southeast Asia, and the Middle East, partnering extensively with 3PL providers and e-commerce fulfillment centers.
 Aliracking